
Flashforge
Flashforge Adventurer 5M
CoreXY · Open frame
220 x 220 x 220 mm build volume
$249.00$309.00
Verified
Last reviewed
The headline mm/s figure on a printer is usually the fastest the tool head can move, not the speed at which it prints clean walls, and some makers list travel and print speeds separately. Real print time depends more on acceleration, hot end flow, cooling and filament, so compare those figures alongside the headline number.
12 printers match this page's criteria with a price verified in the last 24 hours.
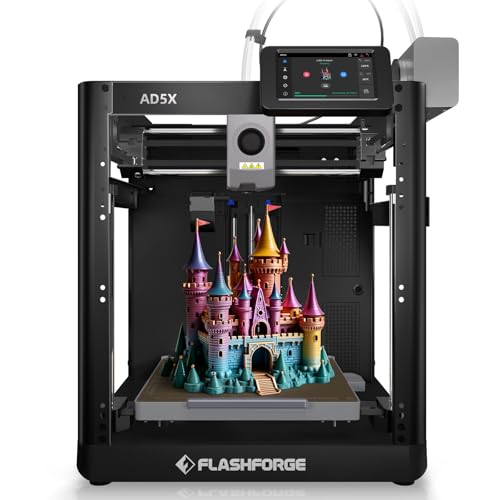
When a maker lists 500 or 600mm/s, it is normally describing the top speed of the tool head. Some say so outright: ELEGOO calls its figure the "max tool head speed" on the Neptune 4 (opens in a new tab), and Bambu Lab uses "max speed of toolhead" on the H2D (opens in a new tab), which it lists at 1,000mm/s. Flashforge goes further on the AD5X (opens in a new tab) and gives two numbers: 600mm/s maximum travel speed and 300mm/s maximum print speed. On the Adventurer 5M (opens in a new tab), the only speed listed is a 600mm/s maximum travel speed.
Travel is the head moving between areas without extruding, so it is bounded only by the motors and frame. Printing is bounded by everything else as well: melting, cooling and the quality of the line laid down. Several makers publish a second, lower figure that is closer to everyday use:
Prusa's product pages list no mm/s figure for the MK4S (opens in a new tab) or the Core One, a reminder that a missing number does not mean a slow printer.
In-stock printers with a manufacturer-stated maximum speed of 500 mm/s or more, fastest stated first. Stated maximums are not print-quality speeds.
Flashforge
CoreXY · Open frame
220 x 220 x 220 mm build volume
$249.00$309.00
Verified
Flashforge
CoreXY
220 x 220 x 220 mm build volume
$349.00$449.00
Verified

Creality
CoreXY · Enclosed · CFS ready
220 x 220 x 250 mm build volume
$368.99$439.00
Verified

Flashforge
CoreXY · Enclosed
220 x 220 x 220 mm build volume
$379.00
Verified

Creality
CoreXY · Enclosed · CFS ready
300 x 300 x 300 mm build volume
$549.00
Verified

Anycubic
CoreXY · Enclosed · ACE Pro ready
250 x 250 x 250 mm build volume
$549.99$649.99
Verified

QIDI
CoreXY · Enclosed
305 x 305 x 280 mm build volume
$699.00
Verified

Creality
CoreXY · Enclosed · CFS ready
350 x 350 x 350 mm build volume
$1,199.00$1,410.99
Verified

Bambu Lab
AMS lite ready
180 x 180 x 180 mm build volume
$249.00
Verified
ELEGOO
CoreXY · Enclosed
256 x 256 x 256 mm build volume
$289.99
Verified

Bambu Lab
AMS lite ready
256 x 256 x 256 mm build volume
$299.99
Verified

Bambu Lab
Enclosed · AMS ready
256 x 256 x 256 mm build volume
$399.00
Verified
| Printer | Build volume | Enclosed | Multi-material | Price |
|---|---|---|---|---|
| Flashforge Adventurer 5M | 220 x 220 x 220 mm | No | Not verified | $249.00 |
| Flashforge AD5X | 220 x 220 x 220 mm | Not verified | Yes | $349.00 |
| Creality K1C | 220 x 220 x 250 mm | Yes | CFS | $368.99 |
| Flashforge Adventurer 5M Pro | 220 x 220 x 220 mm | Yes | None | $379.00 |
| Creality K1 Max | 300 x 300 x 300 mm | Yes | CFS | $549.00 |
| Anycubic Kobra S1 Combo | 250 x 250 x 250 mm | Yes | ACE Pro | $549.99 |
| QIDI Plus4 | 305 x 305 x 280 mm | Yes | Yes | $699.00 |
| Creality K2 Plus Combo | 350 x 350 x 350 mm | Yes | CFS | $1,199.00 |
| Bambu Lab A1 mini with LED lamp kit | 180 x 180 x 180 mm | Not verified | AMS lite | $249.00 |
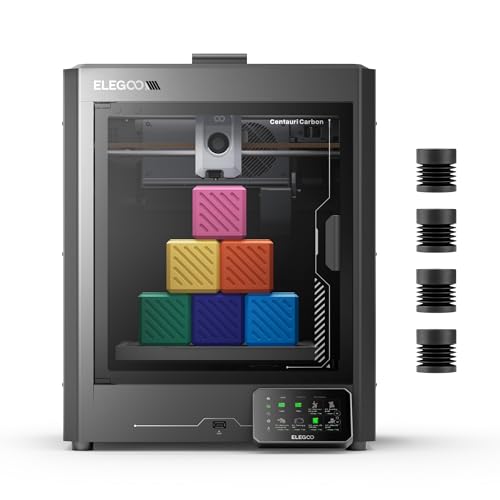
| ELEGOO Centauri Carbon | 256 x 256 x 256 mm | Yes | Yes | $289.99 |
| Bambu Lab A1 | 256 x 256 x 256 mm | Not verified | AMS lite | $299.99 |
| Bambu Lab P1S | 256 x 256 x 256 mm | Yes | AMS | $399.00 |
A print head cannot jump to full speed. It has to accelerate, and then slow down again before every corner. The distance needed to reach a speed from standstill is the speed squared divided by twice the acceleration. Some worked examples:
On a 20mm wide part, a printer with 10,000mm/s² acceleration never reaches 600mm/s at all: the move is over before the climb ends. That is why acceleration often tells you more than top speed for the small and medium parts most people print. A lighter tool head and a stiffer frame allow higher acceleration, and many current machines use vibration compensation (input shaping) in firmware so they can accelerate hard without shaking the frame.
The other hard limit is how much plastic the hot end can melt per second, stated as volumetric flow in mm³/s. A line 0.45mm wide at a 0.2mm layer height has a cross-section of about 0.09mm². At 300mm/s that line needs roughly 27mm³/s; at 600mm/s, roughly 54mm³/s.
Compare that with the flows makers state. Bambu Lab lists 28mm³/s for the A1 (opens in a new tab), ELEGOO lists 32mm³/s for the Centauri Carbon (opens in a new tab), QIDI lists 35mm³/s for the X-Max 3 (opens in a new tab), and Bambu lists 40mm³/s for the H2D's standard hot end and 65mm³/s for its optional high-flow hot end. On those figures, a hot end in the 30mm³/s range supports fine lines somewhere around 300mm/s, not 600mm/s. Thicker lines from a 0.6mm nozzle hit the ceiling at lower speeds. Bambu also states the conditions behind its flow figures, a single-wall model in Bambu ABS at 280°C, which is worth looking for whenever a flow number is quoted.
| Model | Motion | Stated speed | Stated acceleration | Source |
|---|---|---|---|---|
| Sovol SV08 | CoreXY | 700mm/s max | 40,000mm/s² | Sovol (opens in a new tab) |
| Creality K2 Plus | CoreXY | 600mm/s | 30,000mm/s² | Creality (opens in a new tab) |
| Bambu Lab H2D | Not stated | 1,000mm/s tool head | 20,000mm/s² | Bambu Lab (opens in a new tab) |
| Flashforge AD5X | CoreXY | 600 travel, 300 print | 20,000mm/s² | Flashforge (opens in a new tab) |
| Creality Ender-3 V3 | CoreXZ | 600mm/s | 20,000mm/s² | Creality (opens in a new tab) |
| Sovol SV06 Ace | Bed-slinger | 600mm/s max | 20,000mm/s² | Sovol (opens in a new tab) |
| Bambu Lab P1S | Not stated | 500mm/s tool head | 20m/s² (20,000mm/s²) | Bambu Lab (opens in a new tab) |
| Creality Hi | Bed-slinger | 500mm/s, 300 typical | 12,000mm/s² | Creality (opens in a new tab) |
| Bambu Lab A1 | Not stated | 500mm/s tool head | 10,000mm/s² | Bambu Lab (opens in a new tab) |
| Creality Ender-3 V3 KE | Bed-slinger | 500mm/s | 8,000mm/s² | Creality (opens in a new tab) |
Notice that bed-slingers appear with large numbers too. The Sovol SV06 Ace claims the same top speed and acceleration as many CoreXY machines, but moving a heavy bed with a tall part on it is harder than moving a light head, so tall prints usually need gentler settings on an open bed-slinger whatever the spec sheet says.
Pushing a printer toward its stated maximum brings predictable side effects:
Fast slicer profiles handle this by mixing speeds: slower outer walls for appearance, quicker inner walls and infill where nobody looks. Expect most of the time saved to come from infill and travel, not from the visible surfaces.
Standard PLA is formulated for moderate speeds, and many makers say so. Polymaker lists 200mm/s for PolyLite PLA (opens in a new tab) and Prusa lists 200mm/s for Prusament PLA (opens in a new tab). High-speed PLA lines melt more readily: Creality lists 600mm/s for Hyper PLA (opens in a new tab), SUNLU lists 600mm/s for its High Speed PLA (opens in a new tab), and eSUN lists 500mm/s for PLA+HS (opens in a new tab). If you bought a fast printer, a high-speed PLA is what lets it use that speed. The filament finder and best PLA filament pages help match a spool to the machine, and pla.deals compares spools by price per kg, the offer price divided by total net filament weight, with spools of 250g or less labeled samples.
Speed pays off for anyone measuring output in parts per day: prototypers iterating on a design, sellers producing batches, and owners running several machines, covered in our print farm guide. For occasional hobby printing, an overnight print finishing at 4am instead of 7am changes little, and reliability matters more. Printer prices in the grid show when they were verified against Amazon and switch to "Check price at Amazon" after 24 hours.
Rarely. Acceleration, hot end flow, cooling and the filament all cap real speed, and small parts never reach top speed. Typical gains are real but much smaller than the headline ratio suggests.
For most desktop parts, acceleration. Moves are short, so a printer that reaches speed quickly finishes sooner than one with a higher top speed but slower acceleration.
For the fastest profiles, yes. Makers rate standard PLA lines for lower speeds than their high-speed lines, and printing a standard line too fast leads to under-extrusion and weak layers.
It can, especially on outer walls and overhangs. Fast profiles keep visible surfaces slower and speed up infill, which keeps most of the quality while saving time.
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply to the purchase of this product.